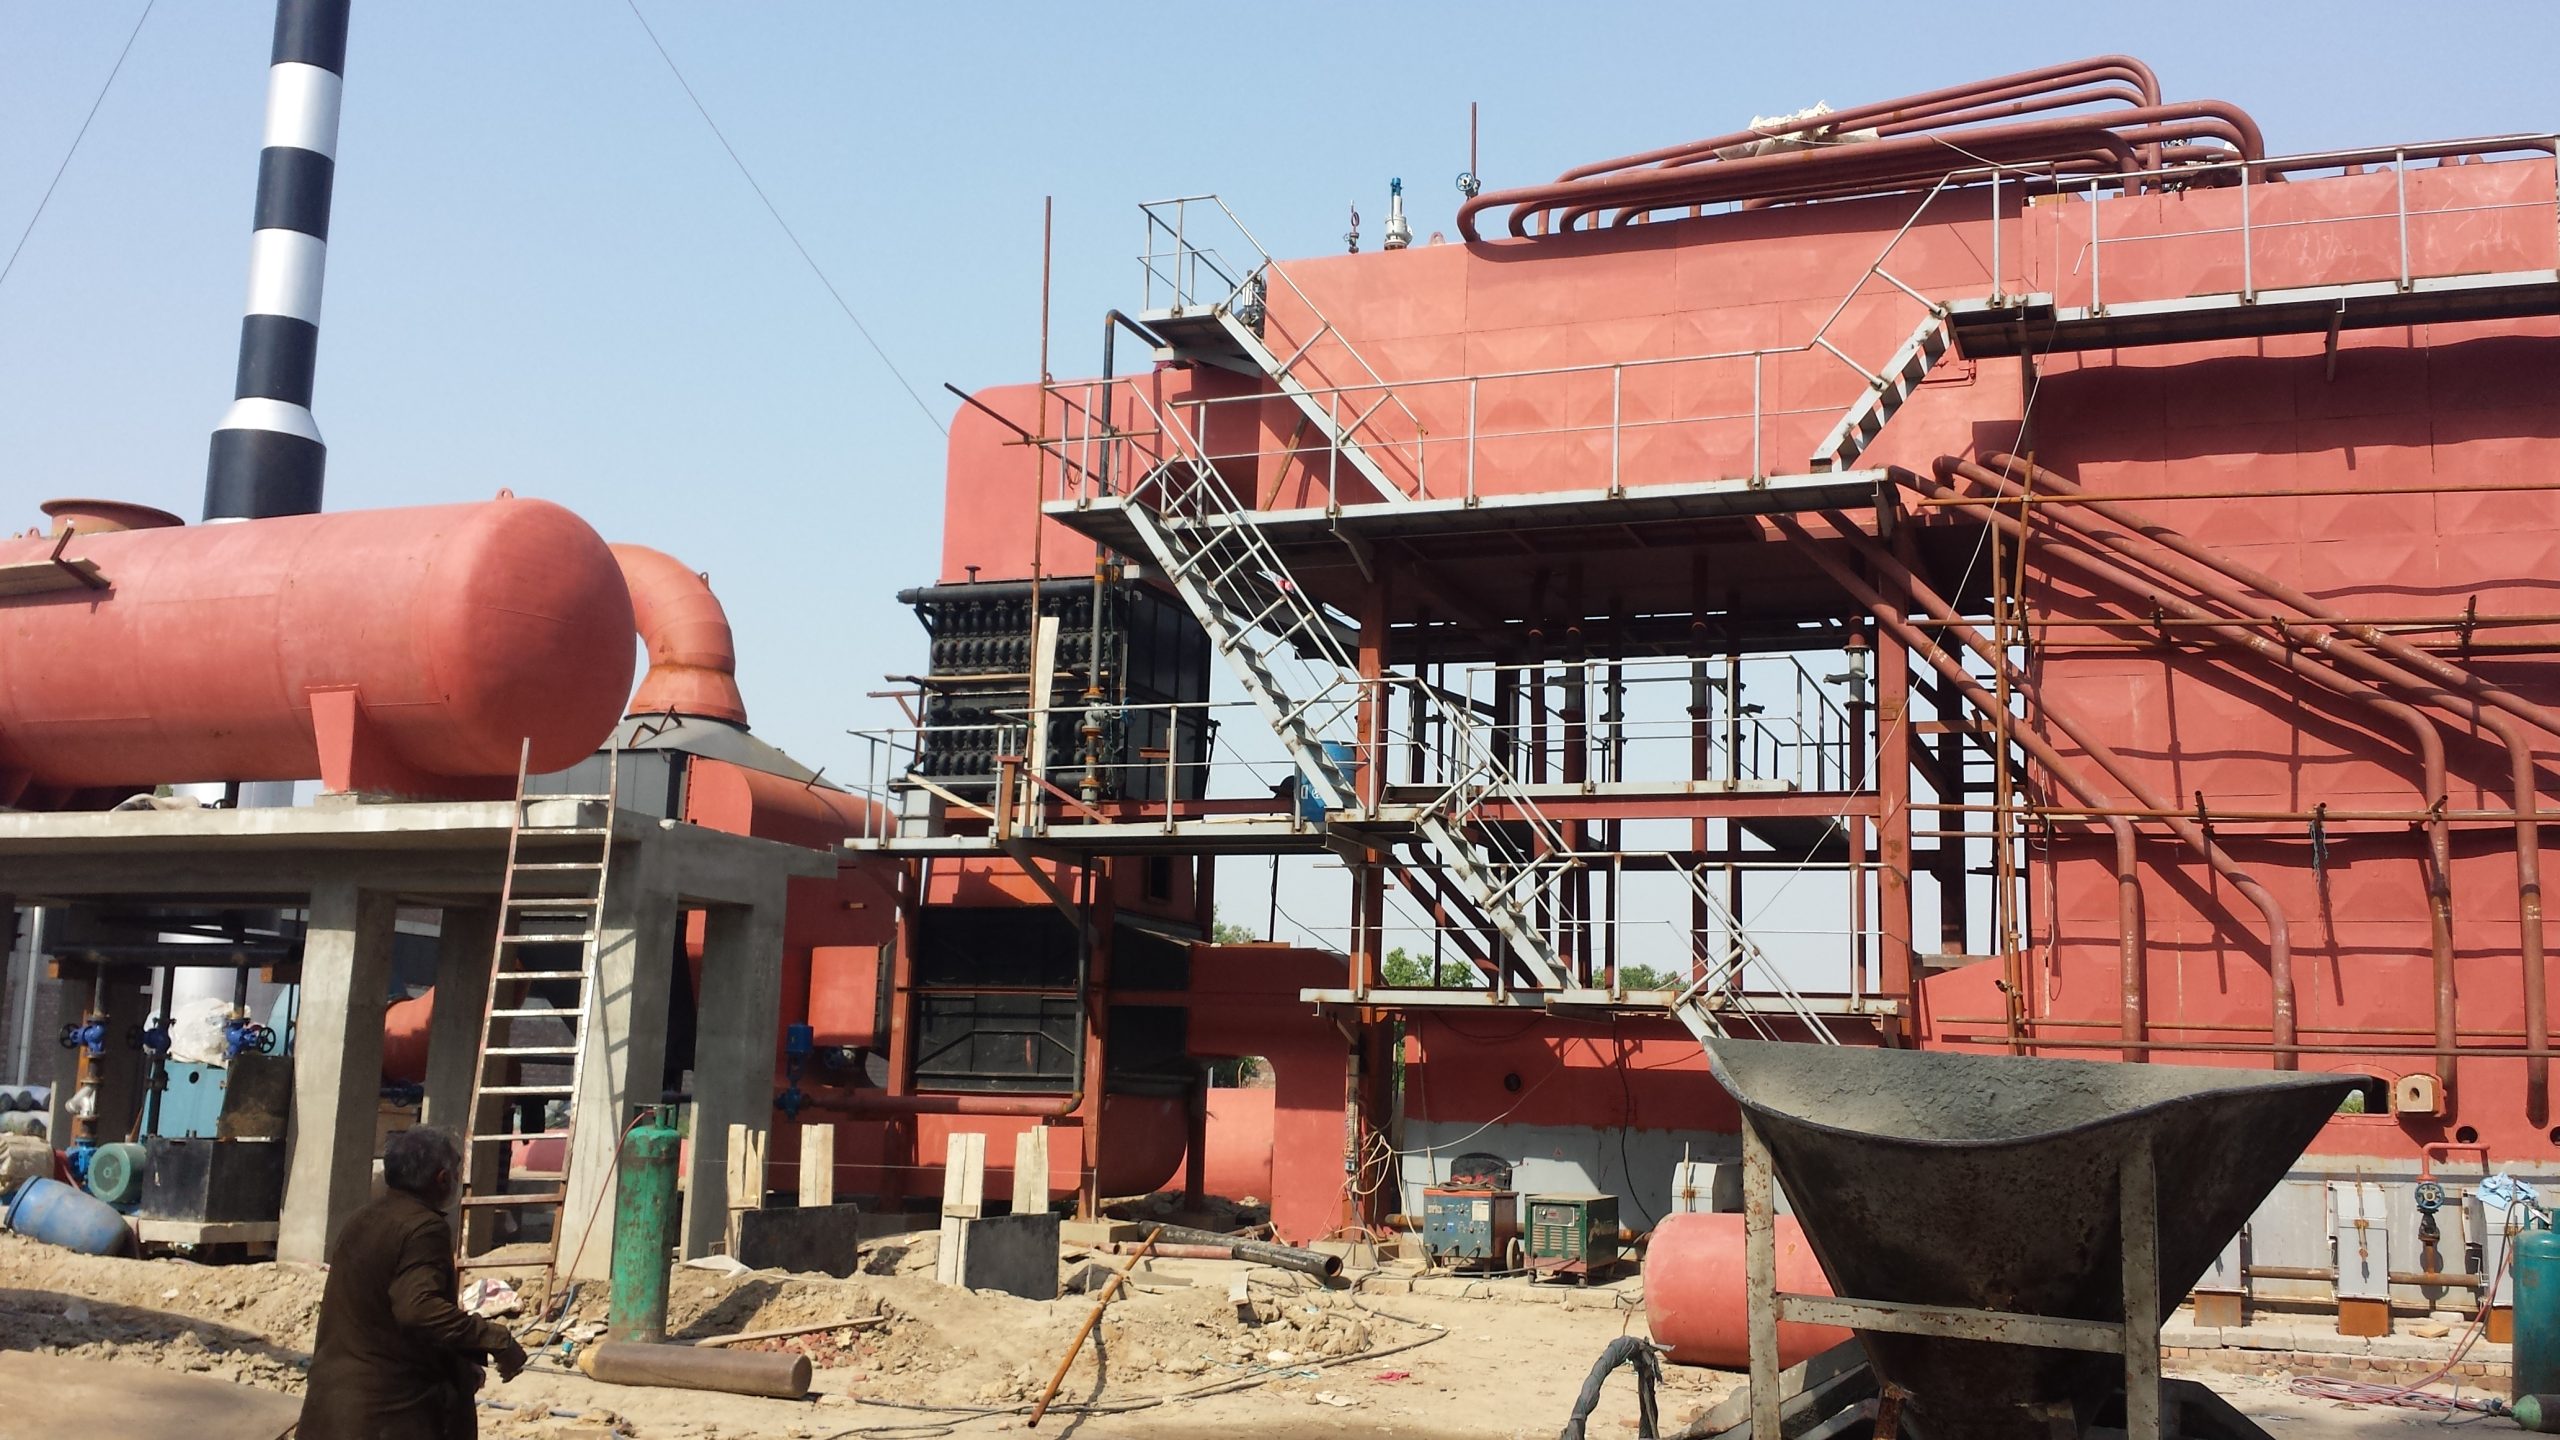
Our Engineering Services
From turnkey fuel conversions to automated control systems and high-purity RO water treatment, we keep your plants operating at peak thermal efficiency.
Fuel Conversion Projects
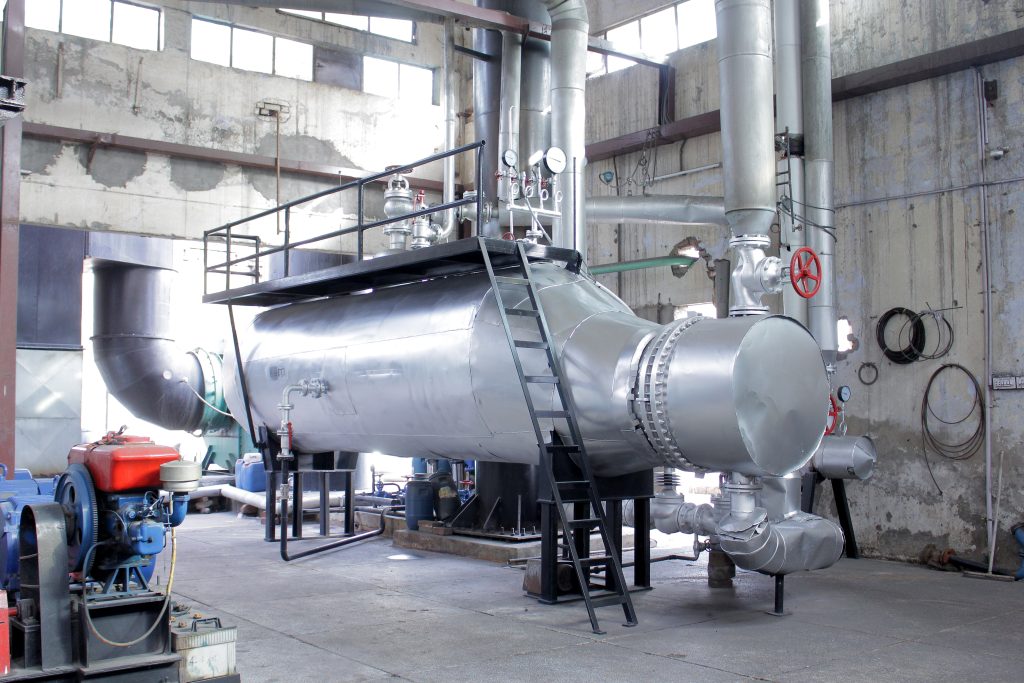
With over 300 successful conversions across Pakistan, STC provides end-to-end fuel retrofit solutions. We engineer and install traveling chain grates, reciprocating step grates, external gasifiers, and fluidized combustion systems that enable your plant to break free from costly imported fossil fuels and gas load-shedding while slashing energy expenditures by up to 40%–60%.
Key Advantages & Performance ROI:
Boiler System Upgrades
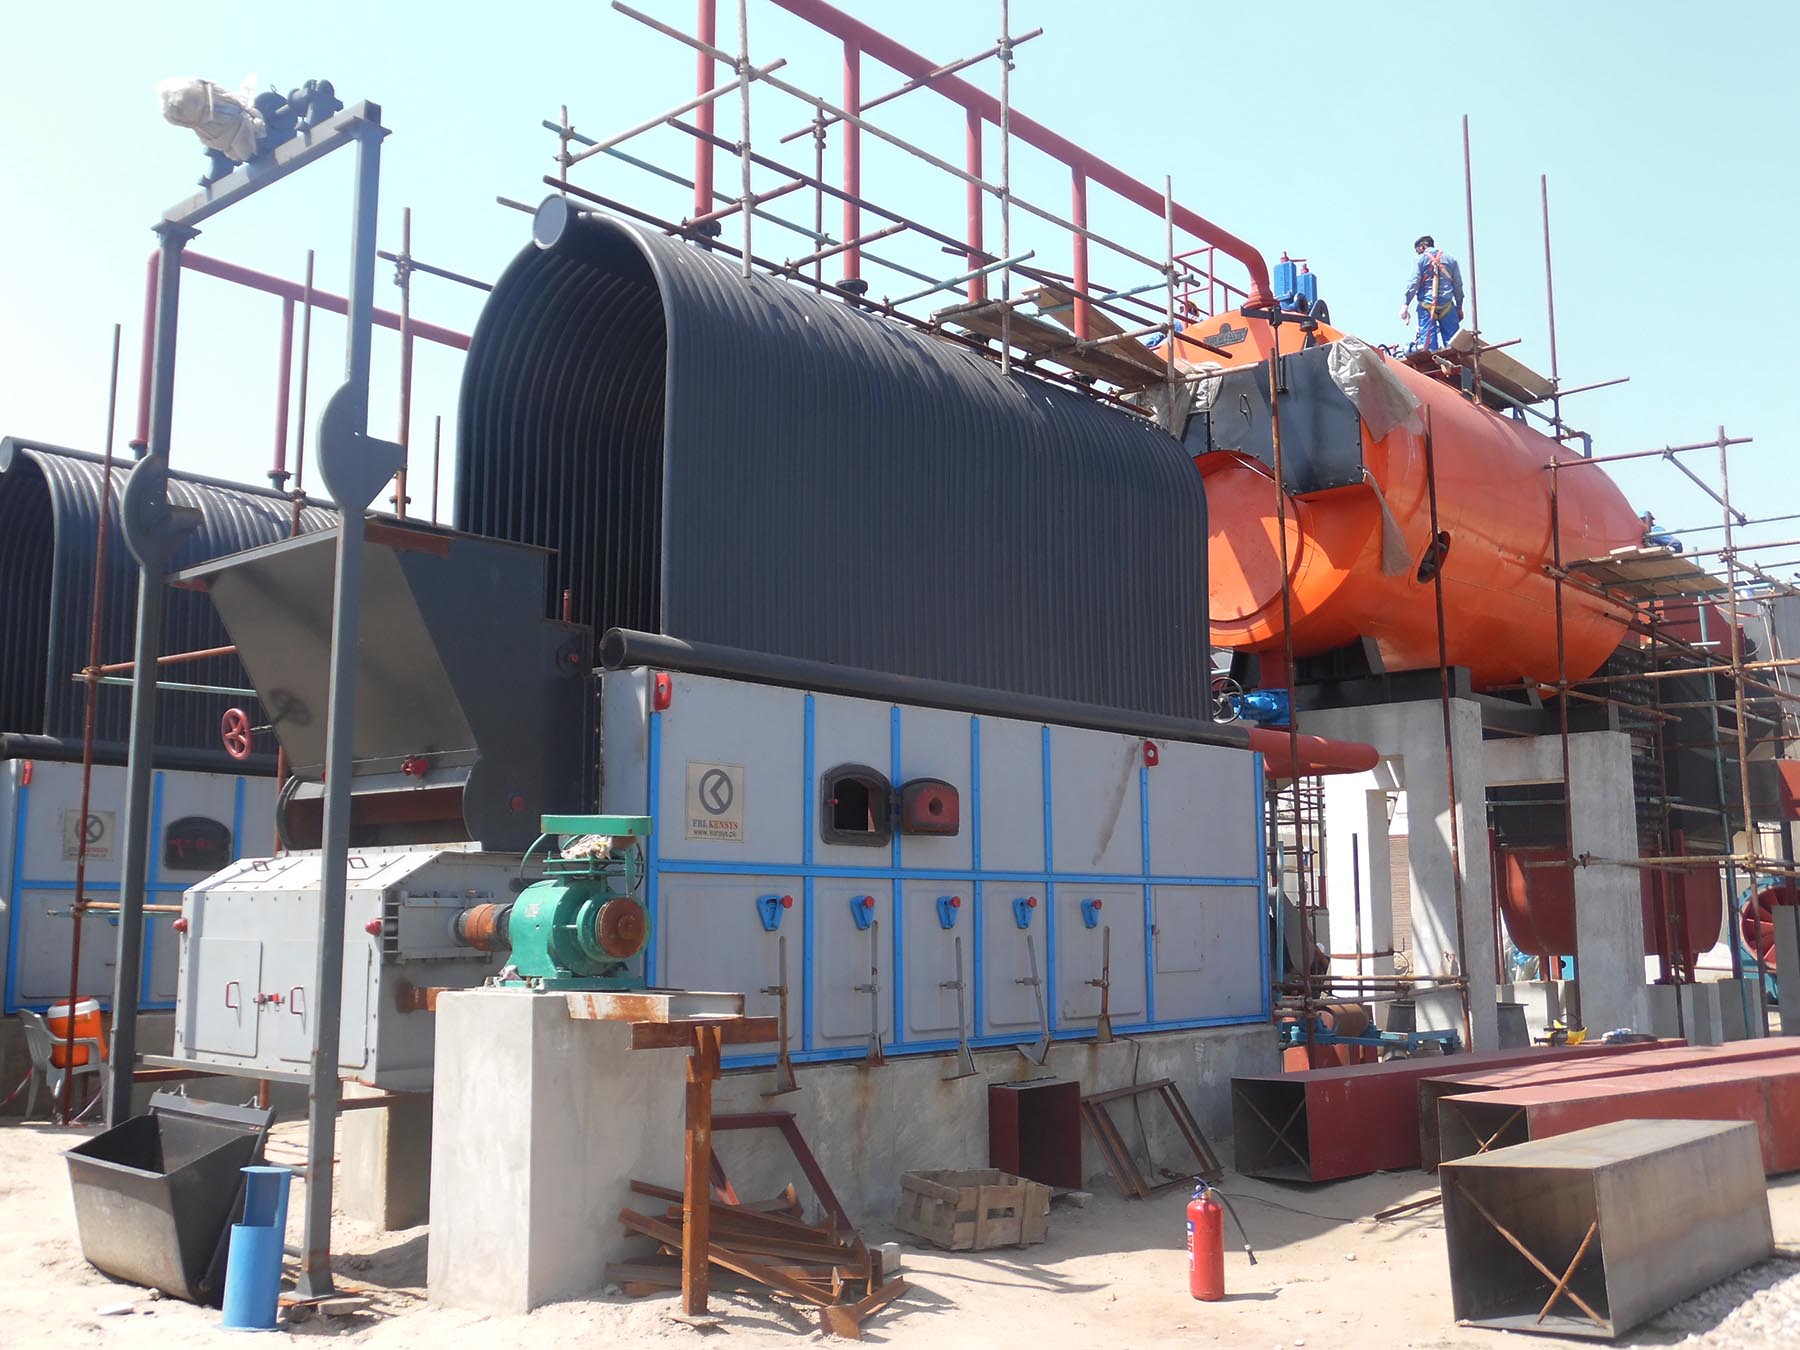
Revitalize aging boiler infrastructure with STC’s advanced upgrade engineering. We retrofit high-efficiency cast-iron and finned-tube economizers, air pre-heaters (APH), automated blowdown controllers, and modern combustion geometry to increase efficiency by 8% to 15% and extend equipment lifespan.
Key Advantages & Performance ROI:
Boiler Spares & Electromechanical Parts
Unplanned downtime is the enemy of industrial profitability. STC maintains a massive inventory of critical boiler spares, including high-grade seamless carbon steel tubes (ASTM A192/BS 3059), heat-resistant alloy grate bars, Mobrey magnetic water level controllers, safety valves, rotary airlocks, and feed pumps.
Key Advantages & Performance ROI:
Industrial Machinery Design & Fabrication
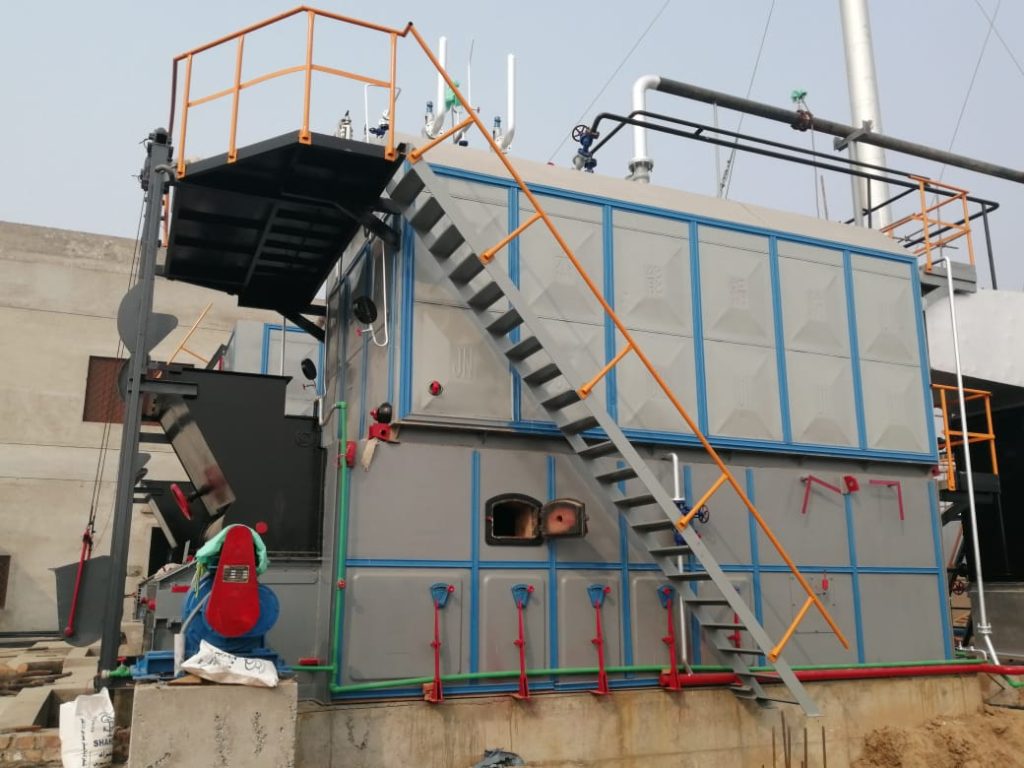
Leveraging our state-of-the-art heavy engineering facility, STC designs and fabricates custom industrial process equipment tailored to exact production requirements. From 1.5 to 10 Ton/hr biomass pelleting plants, heavy-duty rotary dryers, high-RPM hammer mills to cyclone separators and belt conveyors, we build robust machinery made to last.
Key Advantages & Performance ROI:
Industrial Automation & Boiler Panels
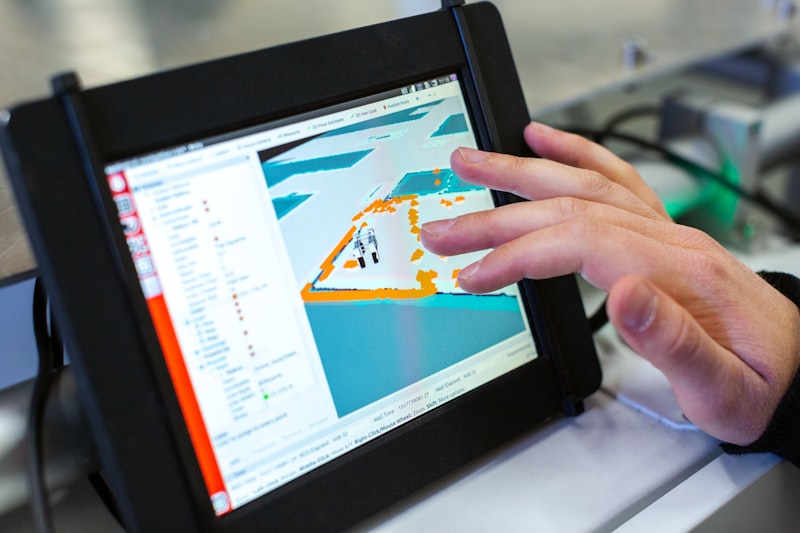
Transform your mechanical boiler into an intelligent, autonomous energy asset. STC designs and builds custom electrical control consoles with Siemens/Schneider PLCs, color touchscreen HMIs, multi-loop PID controllers, and cloud telemetry for real-time monitoring of steam generation, fuel consumption, and emission parameters.
Key Advantages & Performance ROI:
Water Treatment Solutions
Water quality is the single most critical factor in boiler longevity. Even 1mm of scale can reduce boiler heat transfer efficiency by 10% and cause catastrophic tube overheating. STC provides comprehensive water treatment regimens including industrial resin softeners, oxygen scavengers, scale inhibitors, and alkalizing amines.
Key Advantages & Performance ROI:
RO & Demineralization (DM) Plants
For high-pressure boilers, pharmaceutical plants, and sensitive industrial processes, STC manufactures and installs heavy-duty Reverse Osmosis (RO) and Two-Bed/Mixed-Bed Demineralization (DM) plants. Our multi-stage filtration trains remove 99.5% of total dissolved solids, silica, and heavy metal ions.
Key Advantages & Performance ROI:
Industrial Equipment Supply
STC serves as a premier industrial supply partner for leading manufacturing conglomerates. We import and stock an extensive inventory of ASME/DIN certified gate valves, globe valves, thermodynamic steam traps, vortex steam flow meters, level gauges, pressure transmitters, and expansion joints from world-renowned manufacturers.
Key Advantages & Performance ROI:
Ready to Modernize Your Industrial Boiler Systems?
Download our complete technical catalog, biomass pellet specification sheets, and local coal retrofit blueprints, or consult our senior engineering team directly.